If you’ve ever worked with industrial gas cylinders—whether for welding, medical use, or even scuba diving—you know how critical it is to keep them safe. Back when I first started working in our seamless gas cylinder inspection equipment supplier team, I had no clue how much goes into making sure that inspection gear is set up right. Mess up the installation, and you’re not just wasting time and money—you’re putting everyone at risk. Now, after installing hundreds of these systems for clients across the country, I’m breaking down the actual, step-by-step process that we walk through every single time. No fancy jargon, no shortcuts, just the real deal. Seamless Gas Cylinder Inspection Equipment

First off, before we even touch a single bolt, we do a full site walkthrough with the client. This isn’t just a quick “show me where you want it” check-in. We need to measure the space for the inspection line, because seamless gas cylinder testing isn’t something you cram into a tiny corner. For example, some of our bigger automated systems need at least 10 feet of clear space along the cylinder conveyor, plus room on either side for operators to load and unload. We also check the power supply—most of these systems run on 480V three-phase power, not your regular 120V outlet—so we make sure the client’s electrical panel can handle that load. We also ask about their current workflow: do they have a pile of cylinders waiting to be tested right now? How many operators will be working the line? This isn’t just being nosy; it lets us adjust the installation timeline so it fits their schedule without shutting down their whole operation. I once had a client who tried to skip this step and then realized their warehouse floor wasn’t reinforced enough for the heavy inspection tank—we had to push back the install two weeks, which no one wanted. That’s why we never skip the pre-site check.
Next, we get all the pre-install prep out of the way. About a week before we show up, we send a detailed kit list to the client, which includes everything they need to have ready: a flat, level concrete pad (no sloping!) for the main inspection unit, clear access to the drain line for the hydrostatic testing part, and a dedicated disconnect switch for power. We also send over a small checklist of prep tasks, like moving any stored materials out of the installation area so our team doesn’t have to waste time shifting stuff around on day one. One thing we always emphasize here: no modifications to the existing space on their end without running it by us. A client tried to cut a door in a wall to make more space for the system, and it turned out the wall was load-bearing—cost them thousands in repairs, and delayed our install. We’d much rather adjust our system layout to fit their space than have them mess it up themselves.
Once we’re on-site, day one is all about setting up the foundation and roughing in utilities. The main unit is heavy—think like 2,000 pounds for the average system—so we use a forklift or a pallet jack to move it into place, but we never just plop it down. We use a laser level to make sure every corner is perfectly level, within a tolerance of 1/8 of an inch. If it’s even a little off, the cylinder won’t feed straight through the inspection line, which can cause jams and throw off test results. After leveling, we secure the unit to the concrete pad with anchor bolts—no one wants that thing moving if someone bumps it or during a test. Then comes the utility connections: power first, making sure the disconnect switch is properly wired and grounded per OSHA standards. Next is the drain line for hydrostatic testing, which has to be a 2-inch PVC or steel line sloped at least 1/4 inch per foot to prevent water buildup. We also run a compressed air line for the pneumatic parts—like the cylinder grippers and valve actuators—because you can’t run an automated inspection system without that. We test all utilities right after hooking them up: we check for power leaks (the bad kind, not the loose wire kind), make sure the drain flows freely, and test air pressure to make sure it’s steady at 90 PSI. No cutting corners here—if a utility is off, the whole system will crash mid-test.
Day two is when we assemble and calibrate the core inspection components, and this is where most clients are surprised by how meticulous we have to be. Seamless gas cylinder inspection has a few key parts: visual testing, ultrasonic thickness testing, and hydrostatic testing. For ultrasonic testing, which checks for hidden cracks or wall thinning inside the cylinder, we have to calibrate the transducer—basically the sensor that sends and receives sound waves—using a test block that we provide. We run 10 test cylinders of known thickness to make sure the transducer is reading correctly; if it’s even 0.1 mm off, we’ll get bad data, which means a cylinder that’s actually safe might get rejected, or vice versa. Then there’s the visual inspection camera, which is mounted inside the cylinder. We have to adjust the camera angle so it’s centered, no blurriness, and able to scan the entire inner surface of the cylinder in one pass. For the hydrostatic part, we fill the cylinder with water, pressurize it to the required test pressure (usually 5/3 of the working pressure, per DOT regulations), and hold it for a set amount of time. We use a pressure transducer to track any pressure drop, which would mean a leak. But before we even put real cylinders in, we run a dry test with air to make sure the pressure readings are accurate—water can have bubbles that mess with the numbers, so we do a dry run first. I’ve seen new techs skip this and end up with false leak alarms, which meant redoing the whole test at 10 PM. Calibration is non-negotiable.
Once the assembly and calibration are done, day three is all about test runs and operator training. This is when we put the system through its paces with dummy cylinders first. We load a test cylinder (that we know is safe, plus a few that have known defects, like a small crack or thin wall) and run it through the full process. We check if the ultrasonic pick up the defect, if the visual camera sees it, and if the hydrostatic test correctly identifies it. If even one test fails to catch a defect, we go back and adjust the settings—maybe the ultrasonic transducer is a little too far from the cylinder wall, or the pressure hold time is too short. It’s not until every test on the dummy cylinders passes that we move on to training. We don’t just give the client a 10-minute video and dip. We train their operators hands-on, covering loading cylinders, starting a test, reviewing the results, and basic troubleshooting. For example, if a cylinder gets stuck on the conveyor, how to stop the system safely and clear it without breaking anything. We also train their maintenance team on monthly checks—like cleaning the transducer lens, checking air filters, and calibrating the pressure gauge every six months. One client’s operator was nervous about the system at first, so we stayed an extra hour to walk them through three test runs together before we left. That’s part of the job, not an add-on.
Wait, I should mention the little extras that make the install go smooth. We always throw in a pre-install packet with a step-by-step PDF, plus a direct cell number for our lead tech—no generic support line. And during the install, we check in with the client’s site manager every few hours to make sure everything is on track, so they don’t have to wonder what’s going on. We also do a final walkthrough on the last day, going over every function with the whole team, and answer every single question they have—no question is “stupid” here. I once had a client ask if they could test acetylene cylinders with the system, and it turns out we had to adjust the pressure settings for acetylene vs. oxygen, so we fixed that on the spot.
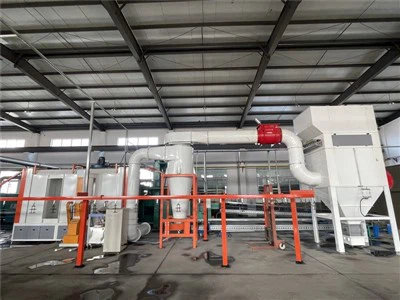
At the end of the day, the seamless gas cylinder inspection equipment installation isn’t just about putting a machine in a room. It’s about making sure that machine works safely, accurately, and fits into the client’s workflow. If you’re a gas cylinder producer, a maintenance shop, or anyone in between that needs to upgrade your inspection setup, don’t risk cutting corners on the install phase. Our team has been doing this for over a decade, and we’ve fixed enough botched installs from other providers to know that taking the time to do it right is always worth it. If you’re ready to stop dealing with unreliable test results and want a system that’s set up correctly from day one, reach out to our team to chat through your needs—we’ll walk you through every step, no pressure, no hidden fees.
Dissolved Acetylene Gas Cylinder Inspection Equipment References
- U.S. Department of Transportation. (2022). Specifications for Transportable Compressed Gas Cylinders. Federal Motor Carrier Safety Administration.
- American Society of Mechanical Engineers. (2021). Boiler and Pressure Vessel Code, Section VIII: Pressure Vessels. ASME International.
- Compressed Gas Association. (2020). Standard for the Qualification of Cylinder Inspection Equipment. CGA G-4.4.
Hangzhou Dongbei Mechanical And Electrical Equipment Co., Ltd.
Hangzhou Dongbei Mechanical And Electrical Equipment Co., Ltd. is one of the most professional seamless gas cylinder inspection equipment manufacturers and suppliers in China. Please feel free to buy high-grade machinery made in China here and get pricelist from our factory. All customized machines are with high quality and low price.
Address: No.6, Gangcheng Shang, Group 15, Sanbaitan Village, Renhe Street, Yuhang District, Hangzhou, Zhejiang Province, China
E-mail: antonioshen@126.com
WebSite: https://www.db-cylinder.com/
